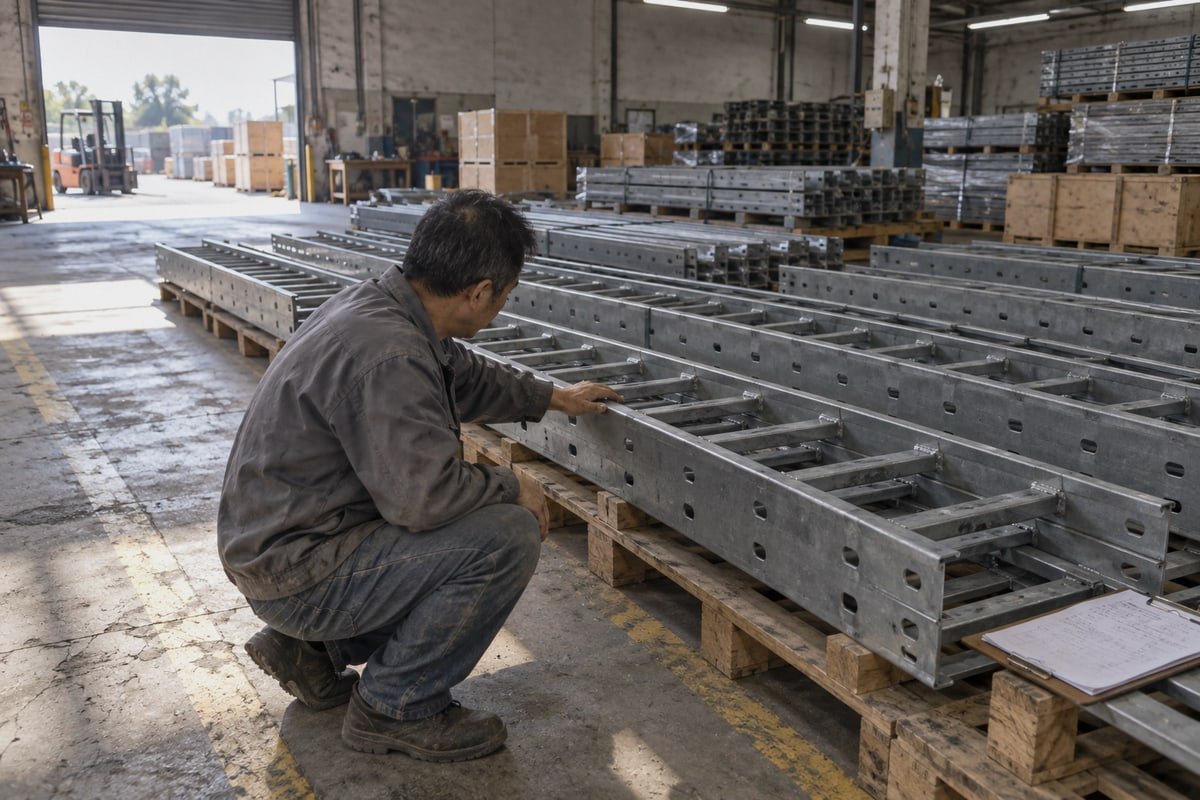
Rusting galvanized trays near a coastal photovoltaic site cost one of our Philippine buyers a full replacement run. That pain pushed our Tai’an team toward the zinc-magnesium-aluminum ladder-type cable tray.
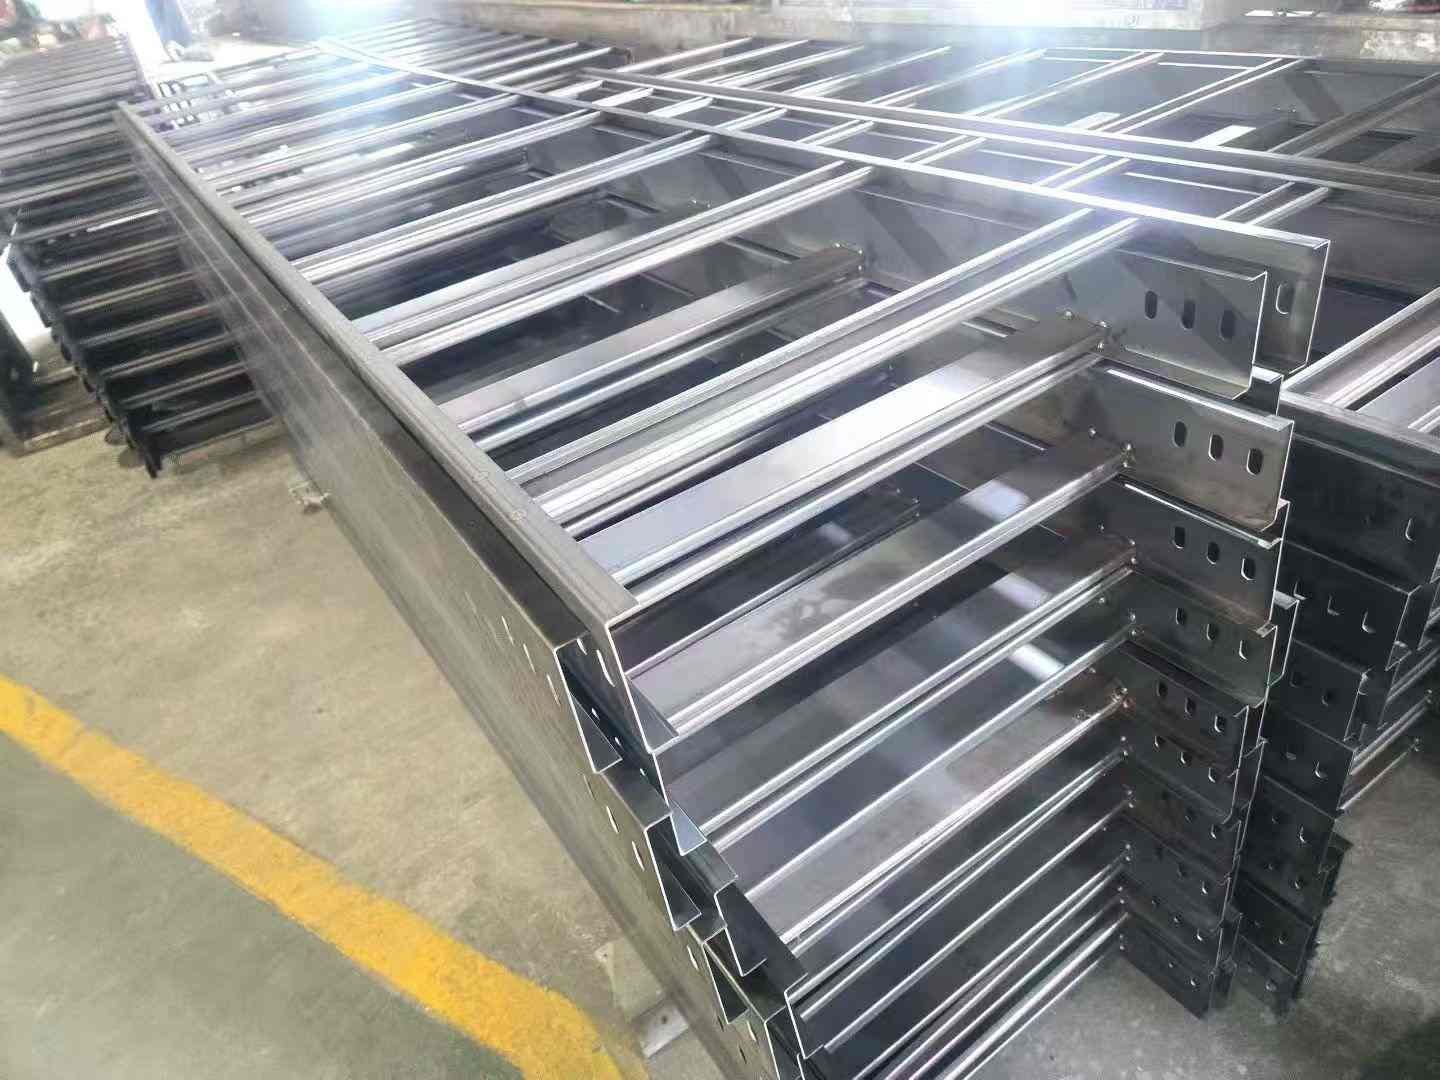
A zinc-magnesium-aluminum ladder-type cable tray is a steel cable support made of two side rails joined by spaced rungs, coated with a zinc-aluminum-magnesium alloy. The open ladder geometry maximizes ventilation and access, while the ZM coating delivers corrosion protection beyond standard hot-dip galvanizing.
The name confuses many buyers. The tray is not a solid exotic alloy. It is steel with a protective metallic skin. The ladder shape and the coating are two separate engineering choices. I will explain both, one at a time, and then show you how to decide if this combination fits your project.
How does zinc-magnesium-aluminum coating improve my cable tray’s corrosion resistance?
During weld checks on our ladder line, I have watched a hot-dip galvanized rung joint show the first rust spots while the ZM joint beside it stayed dull gray.
The zinc-aluminum-magnesium coating improves corrosion resistance in three ways. Zinc corrodes sacrificially instead of the steel. Aluminum forms a stable surface barrier. Magnesium stabilizes dense corrosion products that seal scratches and cut edges. Together they slow rust far longer than plain zinc, especially in chloride and ammonia atmospheres.
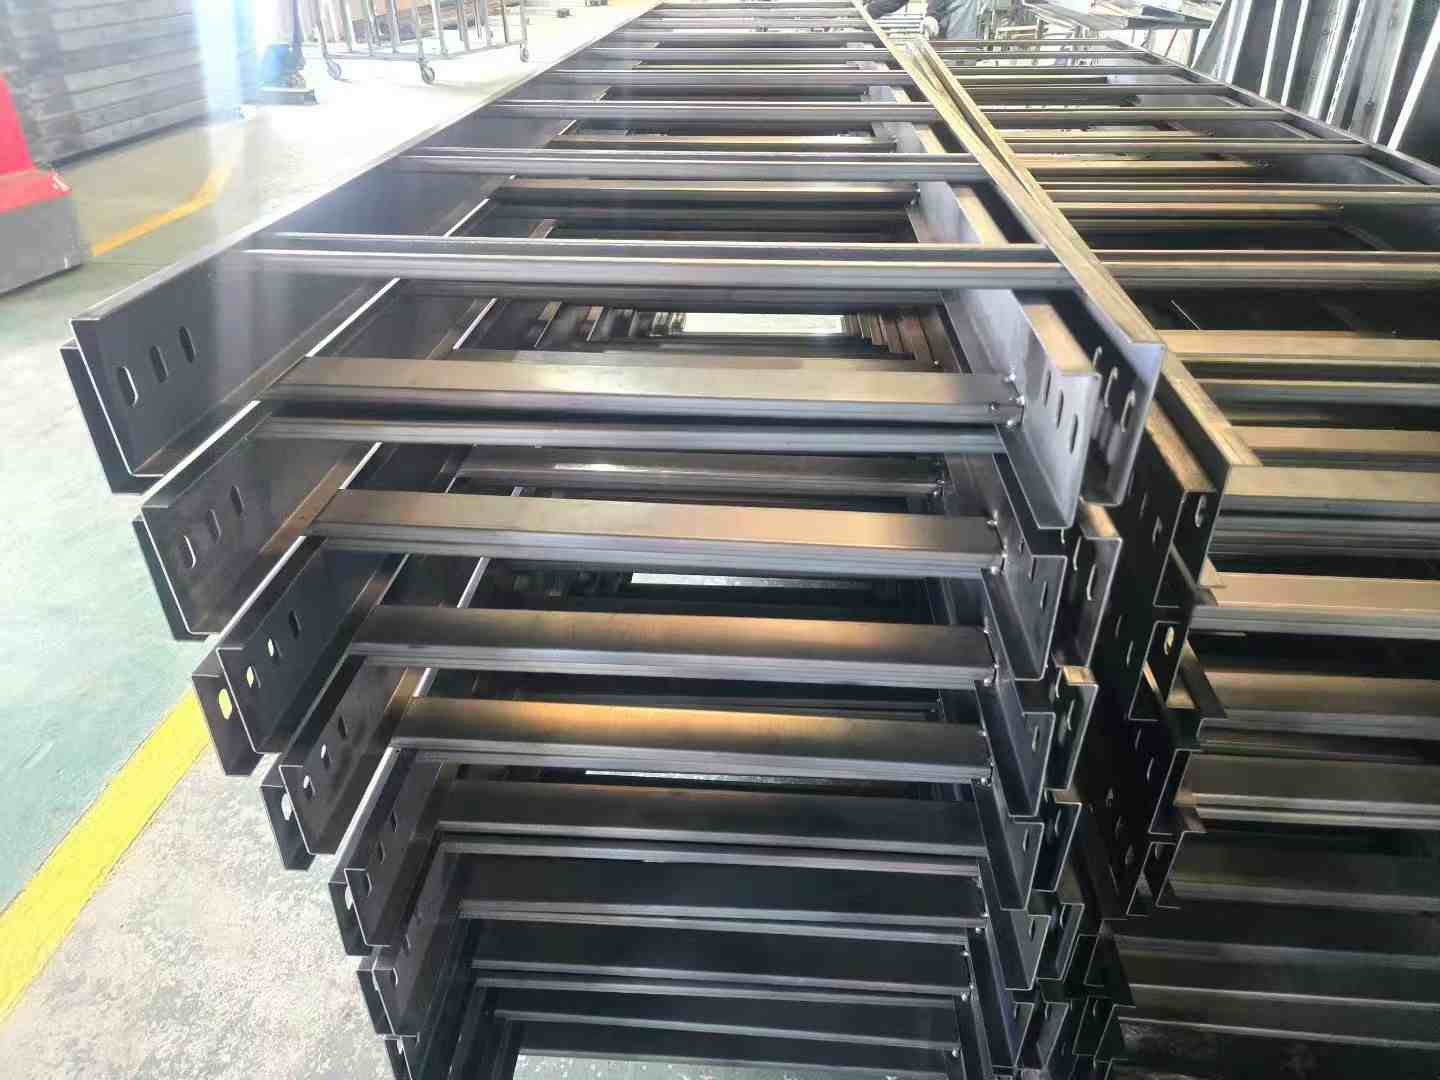
The terms “zinc-magnesium-aluminum”, “zinc-aluminum-magnesium”, “ZM”, “ZAM”, and “ZMA” all point to the same thing. They describe the coating technology, not the body of the tray. The steel underneath does the structural work. The coating does the protection work.
What each element actually does
| Element | Role in the ZMA alloy coating | What it means on site |
|---|---|---|
| Zinc | Sacrificial protection; corrodes before exposed steel | Protects small bare spots and drilled holes |
| Aluminum | Builds a stable, tight surface layer | Better weathering and atmospheric corrosion protection |
| Magnesium | Stabilizes dense corrosion products | Helps cover cut edges and scratches |
Compositions vary between steel mills. One supplier publishes roughly 93.5% zinc, 3.5% aluminum, and 3% magnesium. Other sources describe 5% to 11% aluminum with about 3% magnesium. I always tell buyers to ask for the mill certificate. Do not assume a single universal formula.
Why the rung-to-rail joint matters on a ladder
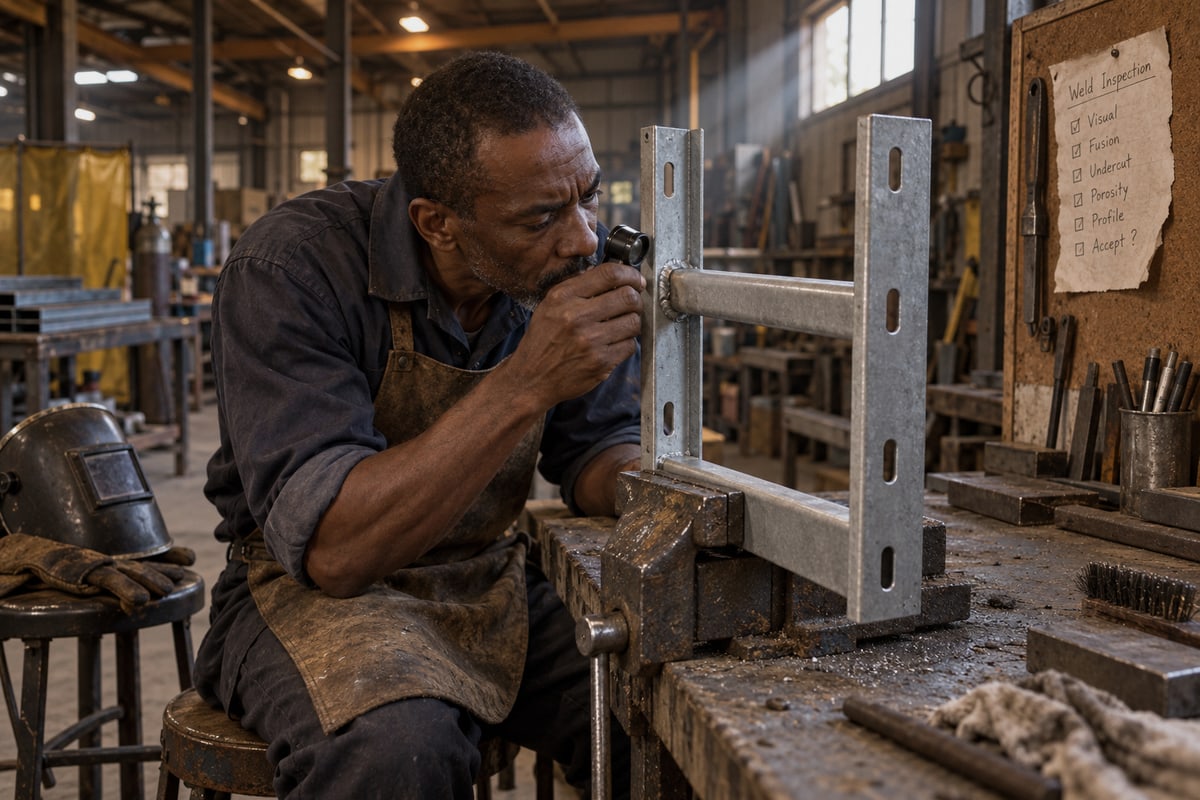
Here is the detail I care about most. On a ladder tray, the rung-to-rail connection is a stress concentration point. It is also where the coating takes the most abuse during forming and welding. With ordinary hot-dip galvanizing 1, the weld heat-affected zone often rusts first. The magnesium in a ZM coating protects these weak points better. But this only works if the welding is clean. A rough, porous weld will fail no matter how good the coating is. That is why our QC on ladder products focuses on the joints, not just the flat surfaces.
What self-healing really means
Suppliers love the phrase “self-healing cut edges”. It is partly true. Corrosion products from the coating can migrate across a small exposed edge and seal it. That is protective re-sealing, not repair. A deep gouge does not grow new steel. A crushed rail does not fix itself. Field-cut ends still need the approved zinc-rich touch-up.
Reading corrosion claims carefully
Some suppliers claim more than three times the corrosion resistance rating of hot-dip galvanized steel in standard environments 2, and up to ten times in chloride or ammonia exposure. Treat these as supplier claims. Ask what salt spray test performance method was used, what baseline product, what coating mass, and what failure criterion. Real service life depends on drainage, temperature, contaminants, fasteners, and installation quality. The coating helps a lot. It does not replace good design.
Why should I choose a ladder-type design over other cable tray styles for my project?
The trade-off I weigh most with the EPC engineers we supply is simple: protection versus heat. A ladder gives up almost all protection to win on cooling, span, and access.
Choose a ladder-type cable tray when cables run hot, need frequent inspection, and face corrosion from air rather than dust or liquid. Open rungs give maximum heat dissipation, longer spans, and cable entry at any point. Avoid it where falling debris, drips, rodents, or shielding are concerns.
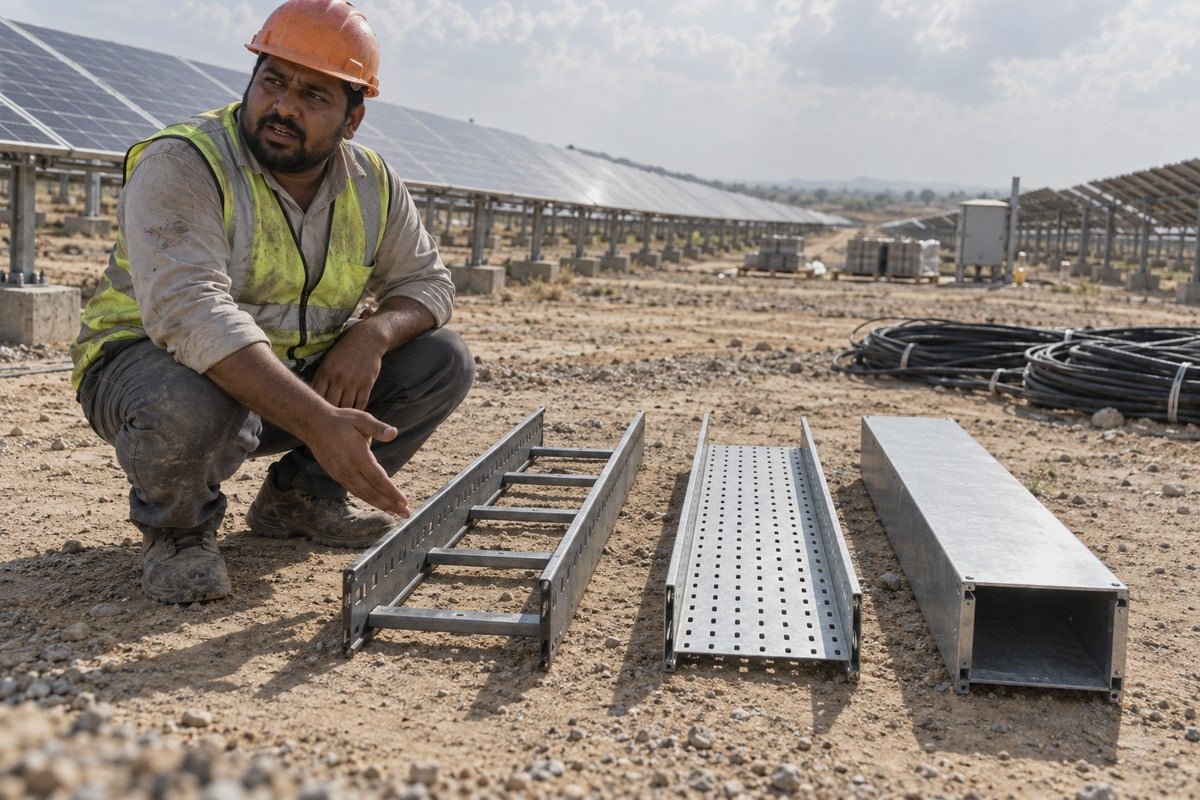
When I put trunking, perforated tray, and ladder side by side, the ladder has the clearest identity of the three. It almost abandons protection. In return it pushes heat dissipation, span length, and maintainability to the limit.
| Tray style | Ventilation | Protection from dust and drips | Typical span | Small-cable support | Best fit |
|---|---|---|---|---|---|
| Ladder-type | Maximum | Almost none | Longest | Needs cleats or ties | Hot power cables, frequent service |
| Perforated tray | Moderate | Partial | Medium | Good | Mixed power and control |
| Solid-bottom / trunking | Low | High | Shorter | Excellent | Small cables, dirty or wet zones |
Where a ladder is the only real answer
Some sites make the choice for you. In photovoltaic power plants, the main DC and AC collector cables carry high current and generate real heat. In substations, power cables need regular inspection. In metallurgy and chemical plants, high-temperature cable channels cannot afford trapped heat. In these places, trunking creates a genuine thermal problem. Perforated tray helps, but the holes are still not open enough. The ladder is the one design that lets air reach most of the cable surface. Typical rung spacing of 150, 225, or 300 mm keeps that airflow while still holding the cables.
One caution. Better ventilation does not automatically raise your cable ampacity 3 on paper. Ampacity still comes from conductor size, insulation, ambient temperature, grouping, and the code tables your engineer must apply.
Where a ladder should not appear
The open structure is not a defect. It is the design premise. If your project has heavy dust, dripping corrosive liquids, rodent pressure, or a need for electromagnetic shielding, the ladder should drop off your option list. Small instrumentation or data cables 4 can sag between rungs or fall through. They need cleats, dividers, or a different tray. Choosing a ladder means accepting the deal: you trade protection for cooling.
Load-bearing capacity and accessibility
The two side rails carry the bending load. The rungs hold the cables and keep the geometry square. This makes the ladder one of the most economical formats for heavy industrial cable support. Cables can enter or exit between any two rungs. Technicians can add or replace circuits without lifting a long cover. For plants that expect expansion, this saves real labor later.
What makes zinc-magnesium-aluminum cable trays a cost-effective choice for my long-term installation?
A project director in Singapore once pushed back on our quotation. Pre-galvanized tray was cheaper per meter, so why pay more for ZM? His question deserved a real answer.
Zinc-magnesium-aluminum cable trays cost more upfront than pre-galvanized steel but less over the installation’s life. Longer service life, fewer replacements, minimal maintenance, protected cut edges, and no post-fabrication dipping reduce total cost of ownership, especially in coastal, industrial, and outdoor sites where galvanized trays fail early.
Price per meter is the wrong number to compare. The right number is cost per year of safe service. Let me walk through how I answered him.
Material options at a glance
| Material or finish | Corrosion performance | Relative cost | Where it fits best |
|---|---|---|---|
| Pre-galvanized steel | Mild indoor only | Lowest | Dry commercial interiors |
| Hot-dip galvanized steel | Good outdoor, thick zinc | Low to mid | Proven general outdoor use |
| ZM / ZAM coated steel | Higher per coating thickness; strong at edges | Mid-range | Coastal, solar, water treatment, industrial |
| Aluminum | Naturally resistant; galvanic risk | Mid to high | Light-weight, long handling runs |
| Stainless steel | Excellent | Highest | Severe chemical, food, washdown |
| FRP (nonmetallic) | Excellent, non-conductive | High | Specific chemical zones |
ZM sits in the middle of this table on cost, which matches how we price it. It is positioned as a hot-dip galvanized alternative, not a stainless steel replacement.
Raising the buyer objection honestly
The objection I hear most is this: “Hot-dip galvanizing is proven. ZM is marketing.” That is a fair challenge. Hot-dip galvanizing remains a solid, widely specified system. It is not wrong to choose it. But two things tilt the decision toward ZM for harsh sites. First, the coating is applied at the mill before forming, so the process skips the energy-intensive secondary dipping and acid pickling stages. That lowers the carbon footprint and often shortens lead time, which matters to the EPC buyers we serve in Southeast Asia and South America. Second, the edge protection reduces the number of early rust points that trigger maintenance calls.
The costs that do not appear on the quotation
Think about what a failed tray really costs. You pay for new material. You pay for scaffolding and labor. You pay for cable handling and possible downtime. In a water treatment plant or a solar farm, that last item dominates. A tray that survives twice as long cuts all of these in half.
Some suppliers also claim ZM’s higher surface hardness resists abrasion during armored cable pulling, and that thinner gauge steel can reach the same load-bearing capacity. I treat those as claims to verify against load tables, not as reasons to reduce rail thickness on a drawing. The same goes for claims about compatibility with low-carbon, high-alkaline concrete. Ask for test data before you rely on it.
My honest summary for that Singapore director was short. If his cables sat indoors and dry, pre-galvanized was fine. His site was coastal and outdoors. ZM paid for itself the first time he did not have to replace a run.
How do I select the right ladder-type cable tray specifications for my specific application?
Our three-person team learned one lesson the hard way: a drawing that only says ZM ladder, 300 mm wide, invites returns. Specifications need load, span, and environment.
Select ladder-type cable tray specifications by defining total cable weight per meter, support span and deflection limit, width and rail height, rung spacing, exposure class, coating mass, bonding method, and required accessories. Then verify everything against the manufacturer’s IEC 61537 load tables and your project’s electrical code.
Returns are the most expensive problem in our business. Almost every return I have handled traced back to a missing line on the specification. So I now walk buyers through a fixed sequence before we cut steel.
A six-step selection sequence
- List the cables. Power, control, instrumentation, fiber, or mixed. Mixed systems may need dividers to control interference.
- Calculate the load. Add up cable weight per meter. Add spare capacity for future circuits. Separate distributed load from point loads, such as a worker stepping on the tray.
- Fix the span. Support spacing sets the rail height and steel thickness. Check the deflection limit on the load table for that exact span, not a shorter one.
- Define the environment. Indoor, outdoor, coastal, washdown, or chemical. Note pH, chlorides, sulfur compounds, ammonia, and temperature. This decides coating mass and whether ZM is enough or stainless is needed.
- Choose accessories. Bends, tees, risers, reducers, covers, cleats, fire barriers, and drop-outs. Confirm fasteners and couplers match the coating.
- Confirm standards. IEC 61537 covers mechanical load, electrical continuity 5, and environmental tests for cable tray and cable ladder systems. Add the national code and any seismic requirement for your jurisdiction.
The checklist I send with every quotation
| Item | Why it matters | Common mistake |
|---|---|---|
| Cable weight per meter | Sets rail height and thickness | Ignoring future additions |
| Span and deflection | Governs load-bearing capacity | Using a short-span table for a long span |
| Rung spacing | Supports small cables, affects airflow | Too wide for instrumentation cables |
| Exposure class | Chooses coating mass | Calling every outdoor site “standard” |
| Bonding method | Equipment grounding continuity | Assuming the tray grounds itself |
| Field-cut repair | Protects exposed edges | No touch-up after on-site drilling |
| Lead time and QC plan | Avoids delays and returns | No weld inspection at the joints |
Two details most buyers miss
First, bonding. A metallic tray can serve as part of the equipment bonding path only when it is joined and installed to the applicable code. That means rated couplers, bonding jumpers where required, and clean joint surfaces. Do not assume it happens by default.
Second, weld quality at the rung-to-rail joint. As I noted earlier, this is where the ZMA coating earns its money, but only on a sound weld. Ask your supplier how they inspect those joints. On our side we photograph them before packing, because that is the one spot where a cheap tray and a good one look identical from a distance.
Conclusion
Rust, heat, and downtime drive most tray failures. A zinc-magnesium-aluminum ladder-type cable tray answers heat and corrosion together, but only when you accept its open design and specify it properly.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
Footnotes
- Authoritative technical resource for the properties and performance of hot-dip galvanizing on steel structures. ↩︎
- ASTM provides international standards for testing metallic coatings in standard environments to evaluate corrosion resistance. ↩︎
- The NFPA publishes the National Electrical Code which defines standards for calculating cable ampacity. ↩︎
- Provides a technical overview of cable tray types, including support requirements for instrumentation or data cables. ↩︎
- Official site for IEC standards covering mechanical load and electrical continuity testing for cable ladders. ↩︎