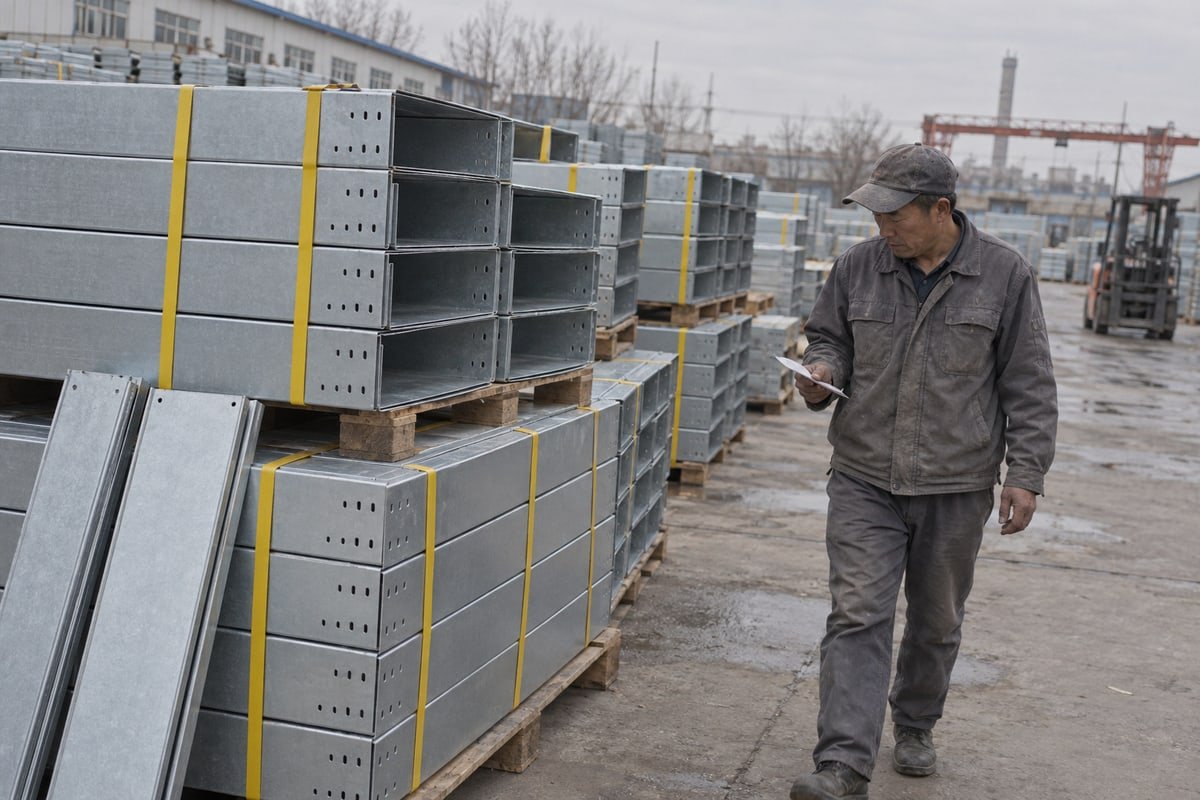
Red rust on a five-year-old tray means shutdowns and angry EPC calls. A zinc-magnesium-aluminum trough-type cable tray exists to prevent that, and our Tai’an line builds them daily.
A zinc-magnesium-aluminum trough-type cable tray is a cable support made from steel sheet coated with a zinc-aluminum-magnesium alloy and formed into a solid-bottom channel, usually with a cover. It carries power, control, and data cables outdoors, targeting 25-plus years of low-maintenance service in corrosive sites.
Two words in that name do two different jobs. “Zinc-magnesium-aluminum” describes the protective alloy coating 1 on the steel. “Trough-type” describes the shape of the channel. I will take each part in turn, then show where this tray earns its keep and where it does not.
How Does Zinc-Magnesium-Aluminum Coating Improve My Cable Tray’s Corrosion Resistance?
Every coil that enters our forming line gets a cut-edge sample tagged and hung on the factory’s outdoor rack. Those edges tell me more than any brochure.
The zinc-aluminum-magnesium coating improves corrosion resistance because zinc corrodes sacrificially, aluminum forms a stable oxide barrier, and magnesium creates dense corrosion products that spread over cut edges and scratches. Together they slow red rust far more than zinc-only galvanizing, especially in salty, humid, or chemical environments.
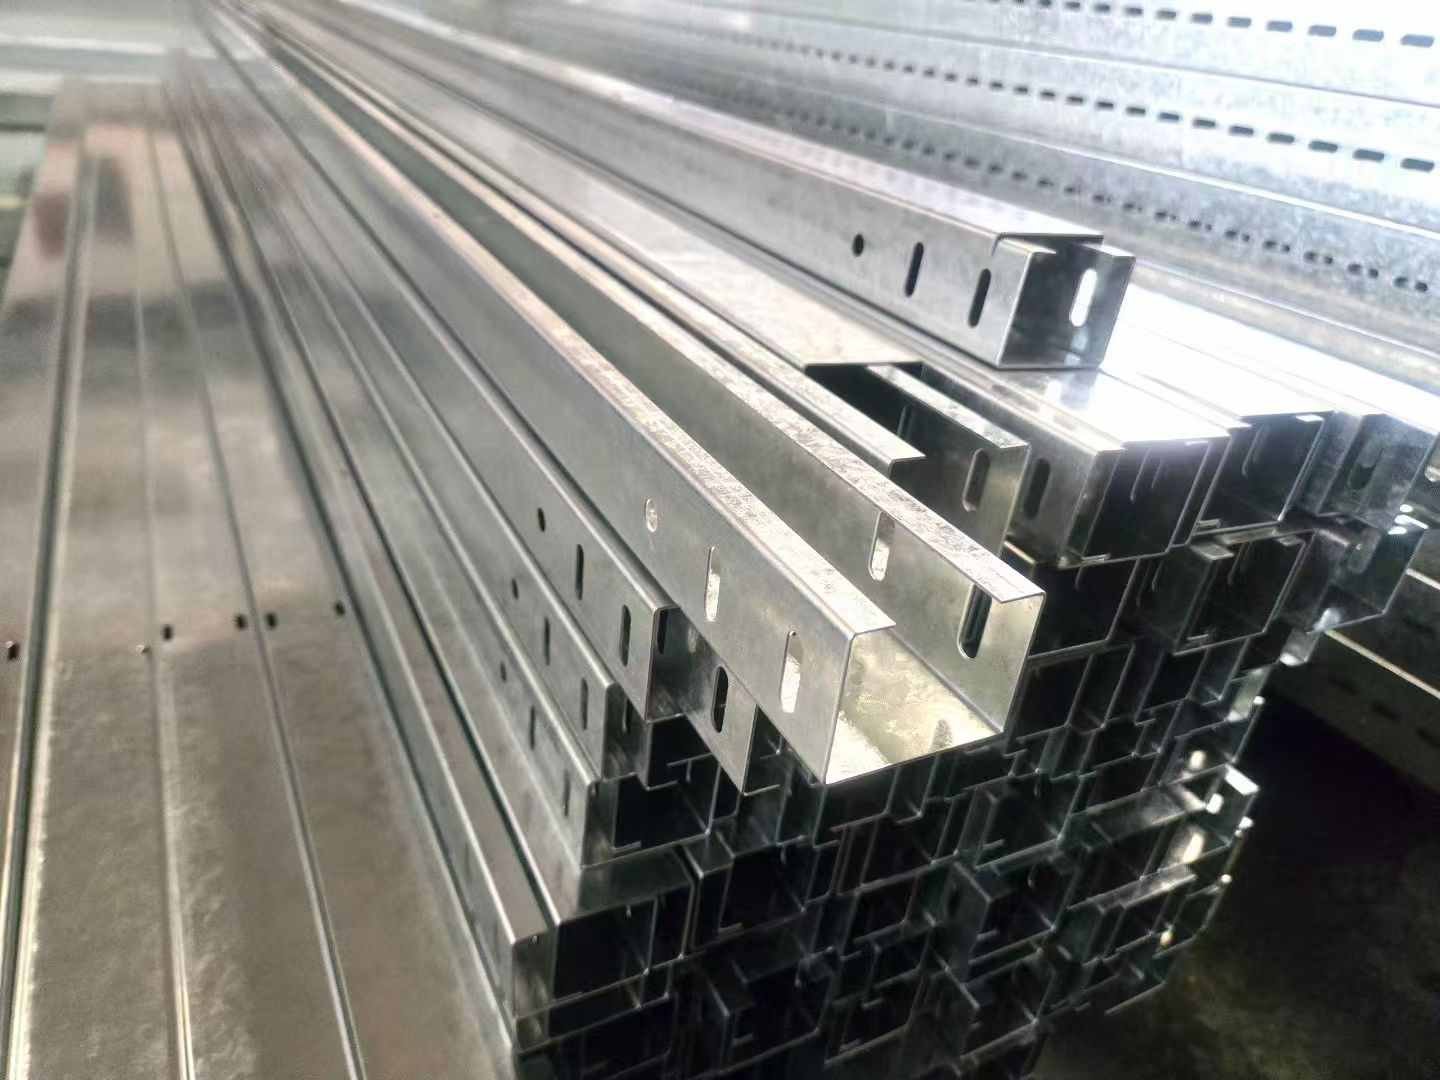
First, a correction I make on almost every first call. The tray is not solid zinc, aluminum, and magnesium. It is cold-rolled steel. The alloy sits on top as a thin metallic layer. The names ZAM, ZM, and Zn-Al-Mg all describe that same layer.
What each metal does inside the protective alloy coating
| Metal | Share in one common recipe | Job in the coating | What you see on site |
|---|---|---|---|
| Zinc | About 93.5% | Sacrificial anode. It corrodes before the steel does. | White deposits instead of red rust |
| Aluminum | About 3.5% | Builds a stable oxide barrier. It slows atmospheric oxidation. | Smooth matte surface with little spangle |
| Magnesium | About 3% | Makes dense, low-conductivity corrosion products that creep over bare steel. | Dark film on sheared edges, no rust creep |
That recipe is one industry example, not a universal rule. Each coil supplier has its own chemistry and coating mass. So I always ask for the coating designation in grams per square metre, not just the word “ZAM”.
Self-healing properties, explained honestly
The magnesium-rich film can migrate onto cut edges, drill holes, and scratches. It forms a protective layer there and slows steel corrosion. That is real, and it is why our field-drilled holes stay clean for years. But the coating does not grow back. It does not restore the original thickness. It does not fix a dent or a crack. So I still tell installers to treat heavy field cuts with the repair compound we ship, and to inspect joints before energization.
Hot-dip galvanized comparison: what the numbers mean
Supplier pages claim three times the corrosion resistance 2 of hot-dip galvanizing in standard air, ten times in chloride, soil, moisture, or ammonia conditions, and some pages even claim 10 to 20 times. I treat every one of those figures as a lab claim until I see the test conditions. A salt spray test shows hours to first red rust under one fixed chloride mist. It does not reproduce a Philippine coastline or a Thai wastewater basin. To compare fairly, you need the reference material, its coating thickness, the exposure duration, and the failure criterion.
What I can state from field experience is simpler. In C4 and C5 environments such as coastal, industrial, or high-humidity sites, conventional hot-dip galvanized tray can show red rust within 5 to 10 years. The ZAM coating is designed around a 25-year maintenance-free target 3 in those same categories. Two more practical benefits come from the continuous hot-dip process on the coil: the surface is smoother than post-fabrication galvanizing, with no uneven spangle, and the alloy is harder, so it resists abrasion when heavy cables are pulled across the bottom.
What Makes a Trough-Type Design Different From Other Cable Tray Styles I Could Choose?
Cover or no cover is the trade-off I weigh most in our quotes. A water treatment client wants drip protection 4; their electrical engineer worries about cable heat. Both are right.
A trough-type cable tray uses a solid or lightly perforated bottom with two upturned side walls, often fitted with a cover. Unlike ladder or wire mesh trays, it gives continuous support and shields cables from dust, drips, and impact, but it ventilates less and needs ampacity checks.
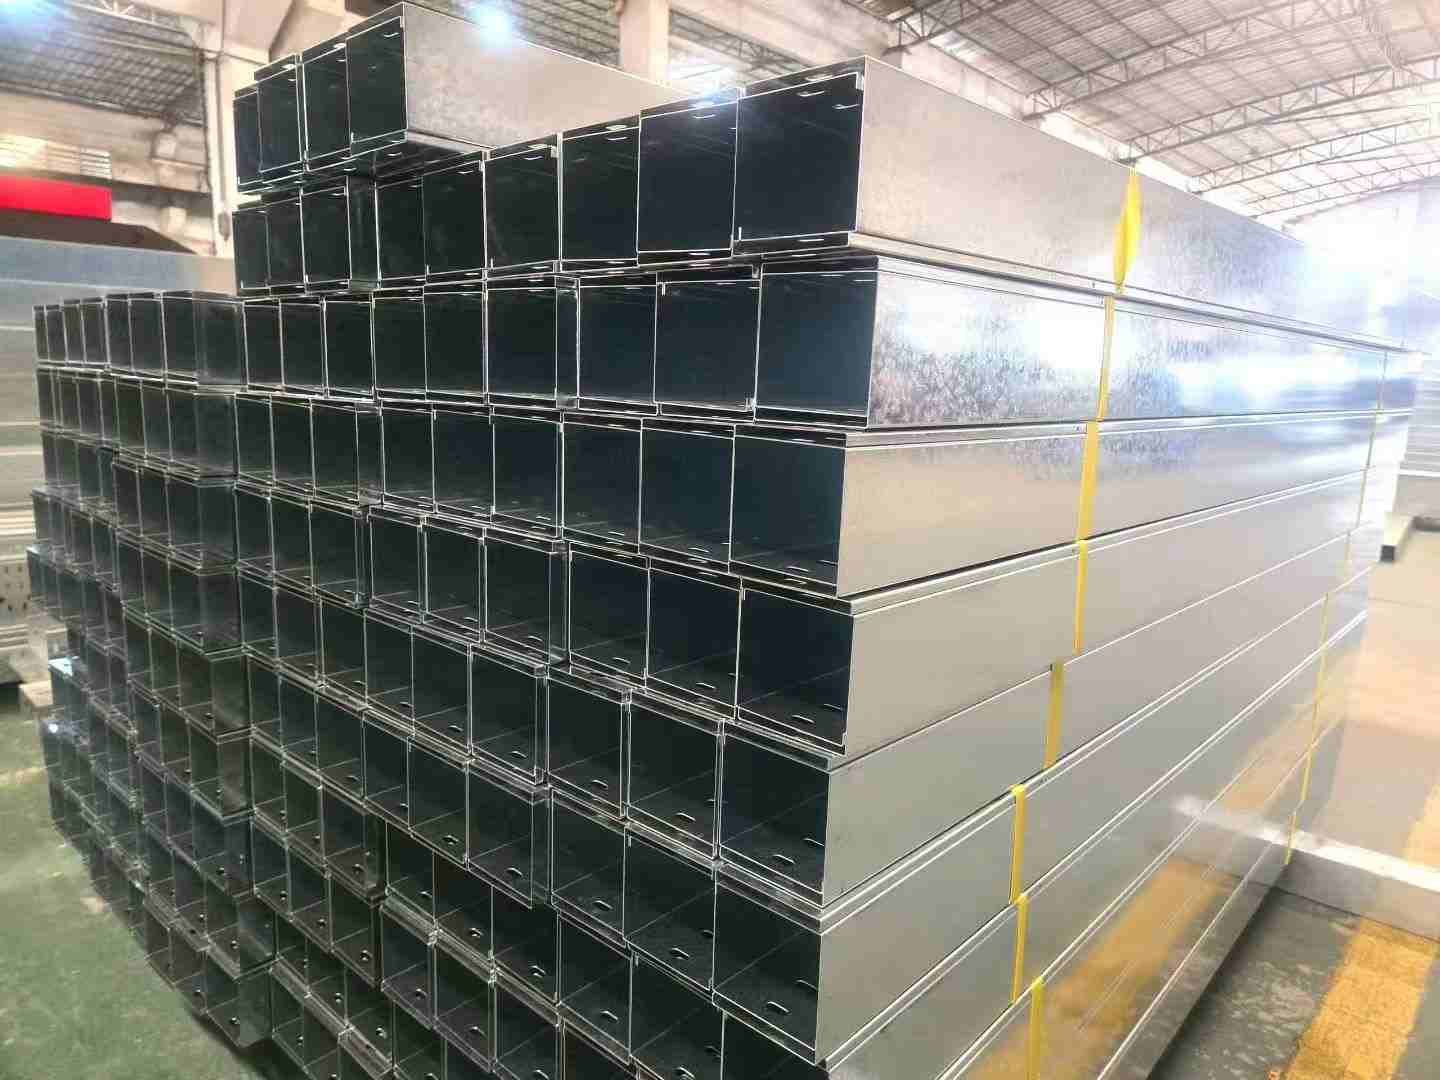
Here is the comparison I send to engineers before we talk price.
| Tray style | Bottom | Ventilation | Shielding from dust and drips | Access for changes | Best fit |
|---|---|---|---|---|---|
| Covered trough (solid bottom design) | Solid sheet | Low | High | Medium, lift the cover | Outdoor PV, water treatment, control and instrument cables |
| Perforated trough | Slotted sheet | Medium | Medium | High | Indoor mixed power and control runs |
| Ladder | Rungs only | High | Low | High | Heavy power cables in plant rooms |
| Wire mesh | Welded wire | High | Low | Very high | Data and light cables in buildings |
| Conduit | Sealed tube | None | Very high | Low | Single runs, hazardous areas |
The trough sits between open ladder and sealed conduit. It is easier to pull, inspect, and expand than conduit. It protects far better than ladder. That middle position is why it dominates industrial cable management in our Southeast Asian projects.
Solid bottom design and cable heat
Power cables make heat. A solid bottom and a cover hold that heat in. So a heavily filled covered trough runs warmer than a ladder tray carrying the same cables. The fix is not to avoid the trough. The fix is to design for it. We ask clients for cable sizes, grouping, ambient temperature, and fill percentage. Then the electrical engineer applies the derating. For small control, instrumentation, and fiber cables, this concern almost disappears, and the continuous support of the bottom is a clear win.
Protection is not an enclosure rating
An open or perforated trough is not watertight or dust-tight. Even a covered one is not sealed unless the joints, cover clips, and fittings are designed and tested for that. Water can enter at couplers. Dust can enter at bends. So in outdoor runs we add drain slots at low points and we discuss mounting orientation before shipping. If your spec calls for a defined ingress-protection level, that level must be verified on the complete assembled system, not assumed from the word “trough”.
Electromagnetic interference shielding
A steel trough with a bonded steel cover forms a partial shield around the cable bundle. It cuts electromagnetic interference 5 reaching data and signal cables more than an open ladder or mesh tray can. Two conditions apply. The sections must be electrically continuous through proper bonding jumpers. And power cables should sit in a separate compartment or a separate tray. We often add a divider for exactly that reason. I do not sell it as a full EMC enclosure; I sell it as a useful improvement that costs very little.
Can I Customize Zinc-Magnesium-Aluminum Trough-Type Cable Trays for My Project’s Specifications?
Last year a Singapore project director sent me a WhatsApp sketch of a non-standard trough with three dividers. Our standard list had nothing close. We built it anyway.
Yes. Zinc-magnesium-aluminum trough-type cable trays can be customized in width, side-wall height, sheet thickness, length, perforation pattern, covers, dividers, fittings, and coating mass. Because the ZAM coating is applied to the coil before forming, OEM/ODM shapes keep the same corrosion protection as standard items.
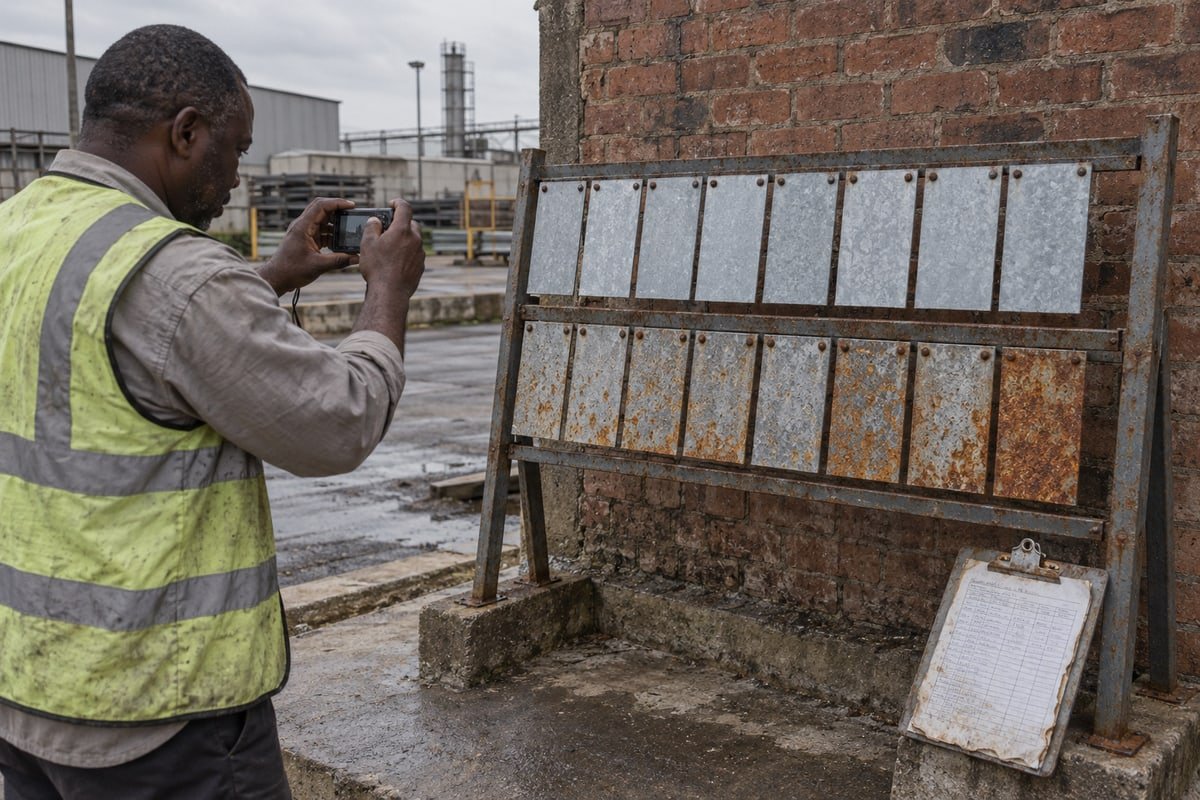
Customization is normal for us because every EPC project has its own drawings. The coating comes on the coil, so changing the shape does not change the surface chemistry. Only the sheared edges differ, and the magnesium-rich film takes care of most of those.
How an OEM/ODM trough order moves through our workshop
- Drawing review. We check width, wall height, span, cable weight, and future expansion against the client’s layout.
- Material selection. We confirm steel grade, sheet thickness, and ZAM coating mass with the coil supplier.
- Forming. The sheet is slit, punched, and roll-formed or brake-formed into the trough profile.
- Fittings. Bends, tees, reducers, risers, splice plates, and C-channel or U-channel support brackets are made from the same coated stock.
- Covers and dividers. Cut to the same length, with slotted perforations for bolting.
- Inspection. Dimensions, coating appearance, edge condition, and hole alignment are checked against the drawing.
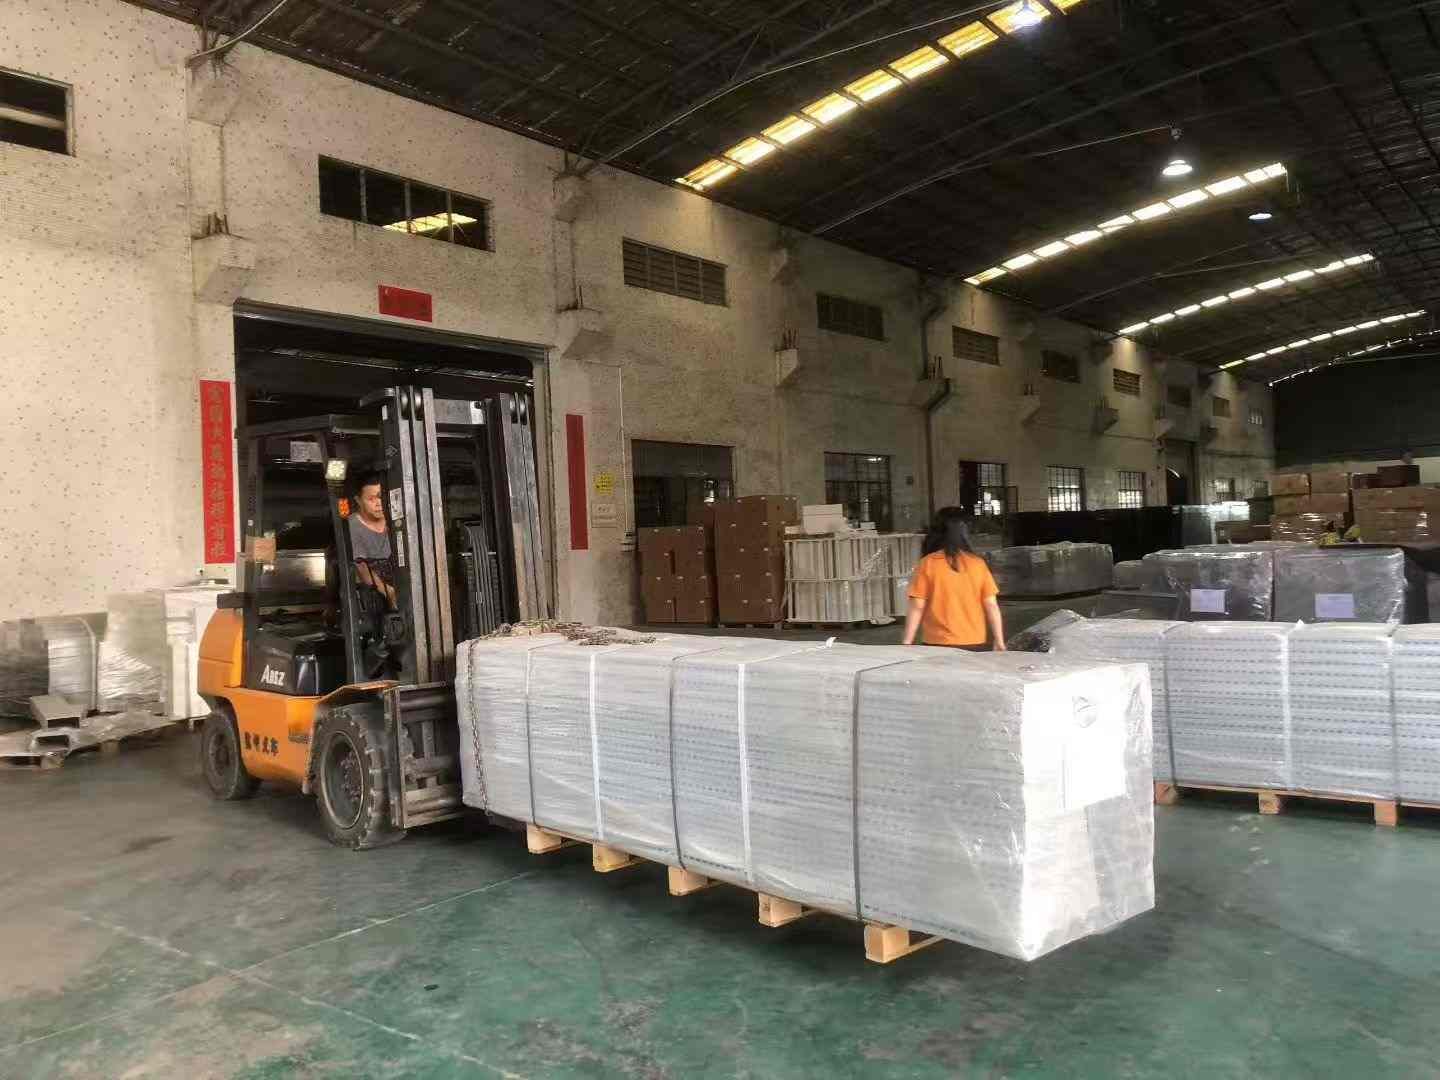
- Packing. Box sections are nested, strapped with yellow bands, stretch-wrapped on timber pallets, and forklift-loaded for container shipping.
What you can specify
| Parameter | Typical options | Why it matters |
|---|---|---|
| Width and side-wall height | Standard steps or custom | Sets cable fill and future spare capacity |
| Sheet thickness | Chosen per span and load | Load capacity comes from steel, not coating |
| Length | Standard or cut to layout | Fewer joints means fewer weak points |
| Bottom pattern | Solid, slotted, perforated | Balances ventilation against shielding |
| Cover | Flat, raised, clipped, bolted | Adds protection and shielding |
| Dividers | One or more compartments | Separates power from data and control |
| Coating mass | Per project corrosivity | Drives service life durability |
| Bonding | Jumpers, continuity plates | Needed for earthing and shielding |
Field cutting and edge treatment
Field drilling, cutting, grinding, and welding expose steel. Small drill holes are fine; the coating protects them. Long grinder cuts and any welding are different. We supply approved cutting tool guidance and a repair compound with each order. We also warn against mixing bare carbon-steel fasteners or untreated timber with the tray in wet areas, because galvanic contact starts corrosion the coating cannot stop.
Lead times and quality control
The pain points I hear most from project directors are late delivery, QC surprises, and returns. A custom tray does not have to cause any of them. We agree the drawing before cutting steel, we photograph each inspection step, and we confirm the packing list by WhatsApp before the container leaves. Our team is small, so one person follows your order from drawing to port.
Why Should I Choose Zinc-Magnesium-Aluminum Trough-Type Cable Trays for My Solar or Water Treatment Project?
My hardest lesson came from a photovoltaic project we quoted that nearly chose ordinary galvanized tray to save pennies. Its 25-year warranty clause changed the whole conversation.
Choose a zinc-magnesium-aluminum trough-type cable tray for solar or water treatment when the site falls in C4 or C5 corrosivity and the asset must run 25 years without tray replacement. Ordinary hot-dip galvanized tray can show red rust in 5–10 years, and mid-life replacement costs exceed any purchase saving.
Photovoltaic power systems are the reason this product spread so fast. A solar plant is sold on a 25-year operating life. The owner, the EPC, and the lender all look at that number. Any component that fails at year eight creates labor cost, lost generation, and contract disputes. The tray is cheap compared to the modules, but replacing it means opening every cable route on site. So the “25-year warranty pressure” pushes the spec toward a coating designed for 25 years of free maintenance.
The price logic is “never replace”, not “buy cheap”
Here is something that surprises buyers. From our quotes, a ZAM trough tray commonly comes in 30 to 50 percent cheaper than a comparable hot-dip galvanized tray, because it skips post-fabrication batch galvanizing and uses a thinner coated sheet. Against basic electro-galvanized tray, yes, it can cost more. But neither comparison is the point. The point is that you buy once and do not come back. Some supplier pages claim 30 to 50 years of service life; I prefer to promise the 25-year design target and let the site prove the rest.
| Option | Purchase price position | Performance in C4/C5 sites | Expected maintenance | When I recommend it |
|---|---|---|---|---|
| Electro-galvanized steel | Lowest | Poor, thin coating | High outdoors | Dry indoor only |
| Hot-dip galvanized steel | Higher than ZAM | Red rust possible in 5–10 years | Touch-up, possible replacement | Where thick zinc is specified and site is mild |
| Zn-Al-Mg trough (ZAM) | Mid-range | Designed for 25-year maintenance-free target | Inspect edges and drains | Solar, coastal, wastewater, humid industrial |
| Stainless steel | Highest | Excellent | Very low | Food, pharma, extreme chemical splash |
| FRP | Mid to high | Excellent chemical resistance | Check UV and impact | Non-conductive or acid-fume zones |
Water treatment: humidity, chlorine, and ammonia
Wastewater plants combine constant humidity 6 with chlorine, ammonia, and sulfur gases. Those are the exact conditions where supplier data shows the largest gap between ZAM and plain zinc. A covered trough also keeps spray and sludge off the cables. I pair it with dividers for instrumentation, drain slots at low points, and stainless or coated fasteners matched to the environment.
When I tell a client not to buy it
I would be a poor partner if I called this tray universal. In a dry, air-conditioned plant room, standard galvanized tray is adequate, and the extra coating buys nothing. In a chemical plant with direct acid splash, stainless steel or FRP is the safer call. Where heavy power cables need maximum heat dissipation, a ZAM ladder tray may beat a ZAM trough. And no coating rescues a tray with poor drainage, trapped contaminants, or overload.
What to verify before signing
Do not pick a tray by coating name alone. Ask for the coating composition and mass, the steel grade and thickness, the load rating at your proposed span, the deflection limit, and whether the whole system or only the sheet was tested. Check your national electrical code, the corrosivity category, earthing rules, and fire requirements. A thinner ZAM sheet can carry the same load as a thicker older design, which lightens handling and lowers carbon in production, but only if the span and support spacing were engineered for it.
Conclusion
Rust forces replacement; replacement forces shutdowns. A zinc-magnesium-aluminum trough-type cable tray avoids both where corrosion is real. Message me, and we will size one for your site.
Footnotes
- ASTM International defines technical specifications for protective alloy coatings like zinc-aluminum-magnesium on steel products. ↩︎
- ISO provides international standards for evaluating the corrosion resistance of metallic coatings in various environments. ↩︎
- Wikipedia explains the longevity and maintenance-free characteristics of hot-dip metallic coatings on steel. ↩︎
- IEEE standards cover the design and environmental protection requirements for industrial cable management systems. ↩︎
- Authoritative Wikipedia entry defining EMI and its shielding principles. ↩︎
- The EPA provides guidance on managing infrastructure in wastewater environments characterized by constant humidity and corrosive gases. ↩︎