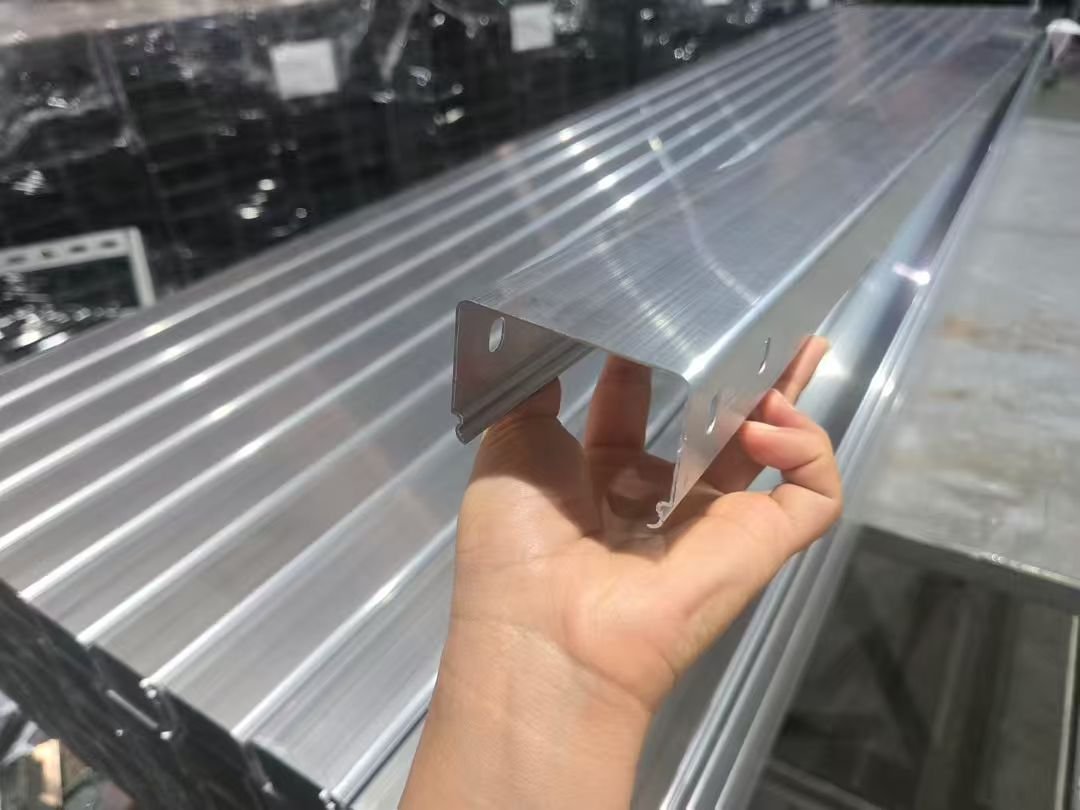
Crews on a Singapore solar site once lost two days re-tightening loose splice bolts. That pain pushed our Tai’an factory to refine the self-locking aluminum alloy cable tray.
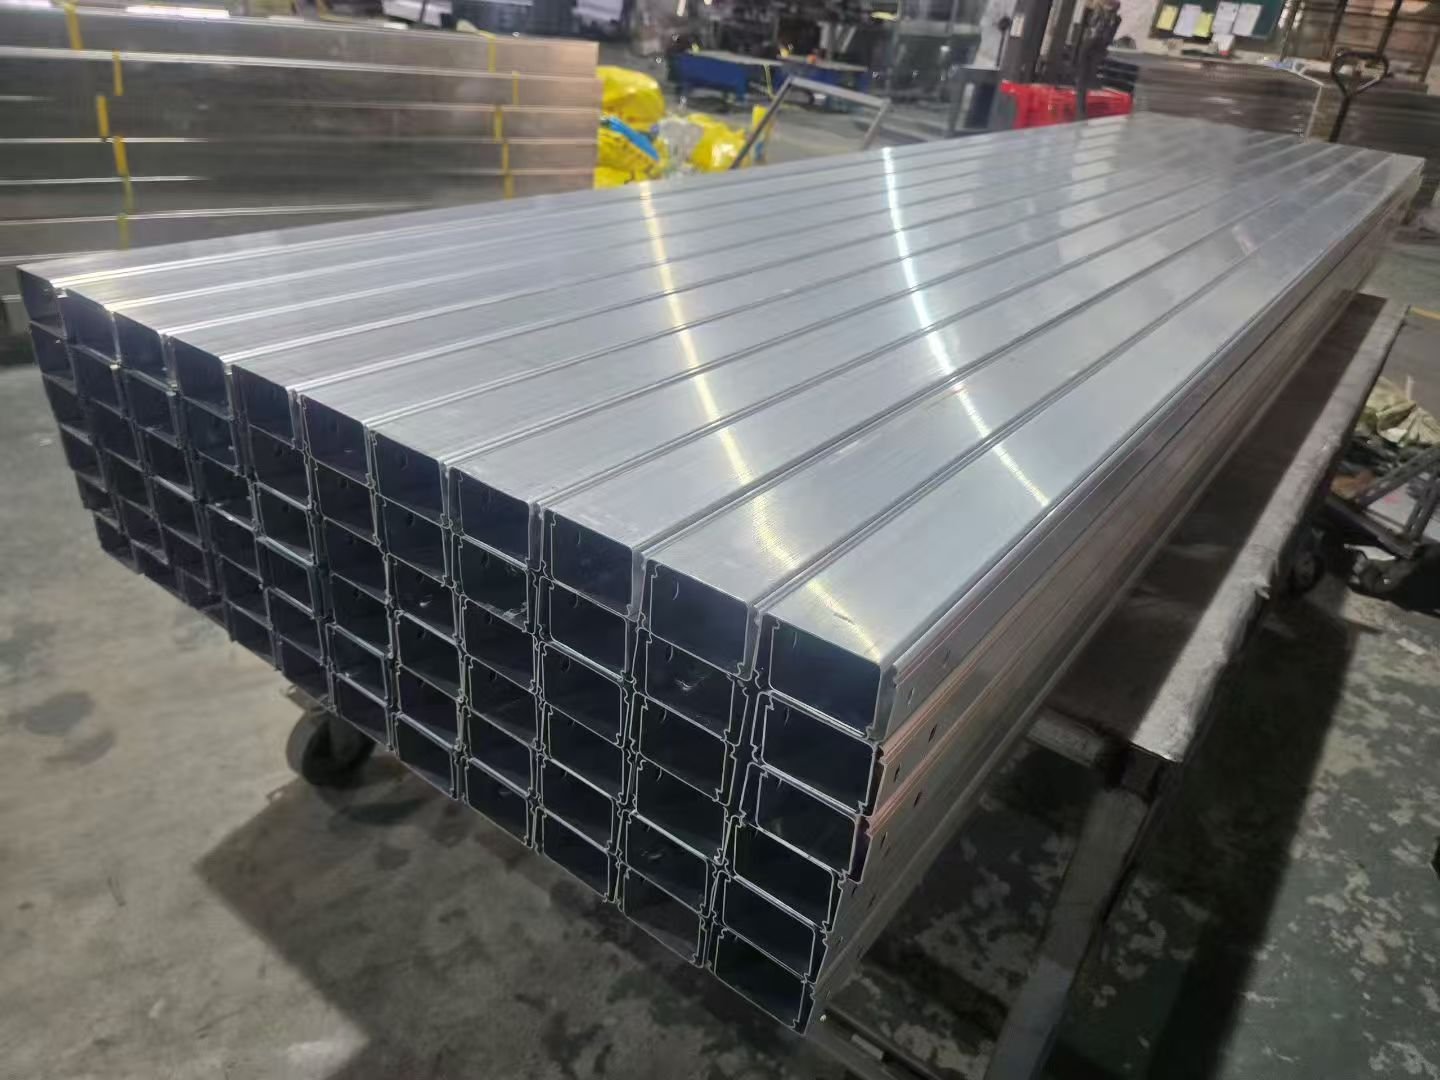
A self-locking aluminum alloy cable tray is a cable management system whose extruded aluminum sections join through snap-fit or slide-lock profiles instead of bolts and splice plates. The geometry of the joint holds sections together, cutting installation time while keeping aluminum’s light weight and corrosion resistance.
That is the short answer. But the details matter a lot before you buy. Below, I will explain how the lock works, where it beats bolted trays, where it does not, and how to pick a supplier who can actually make it right.
How does a self-locking aluminum alloy cable tray actually work?
Last spring, our QC team rejected a batch of extruded profiles because the locking groove ran slightly oversize. That small error taught me exactly how this mechanism works.
The tray works through shaped extruded profiles. Installers align two sections, then slide or press them together. A slider passes a sloping section, drops into a locking hole, and an anti-locking section stops reverse movement. The joint holds itself through geometry, not bolts.
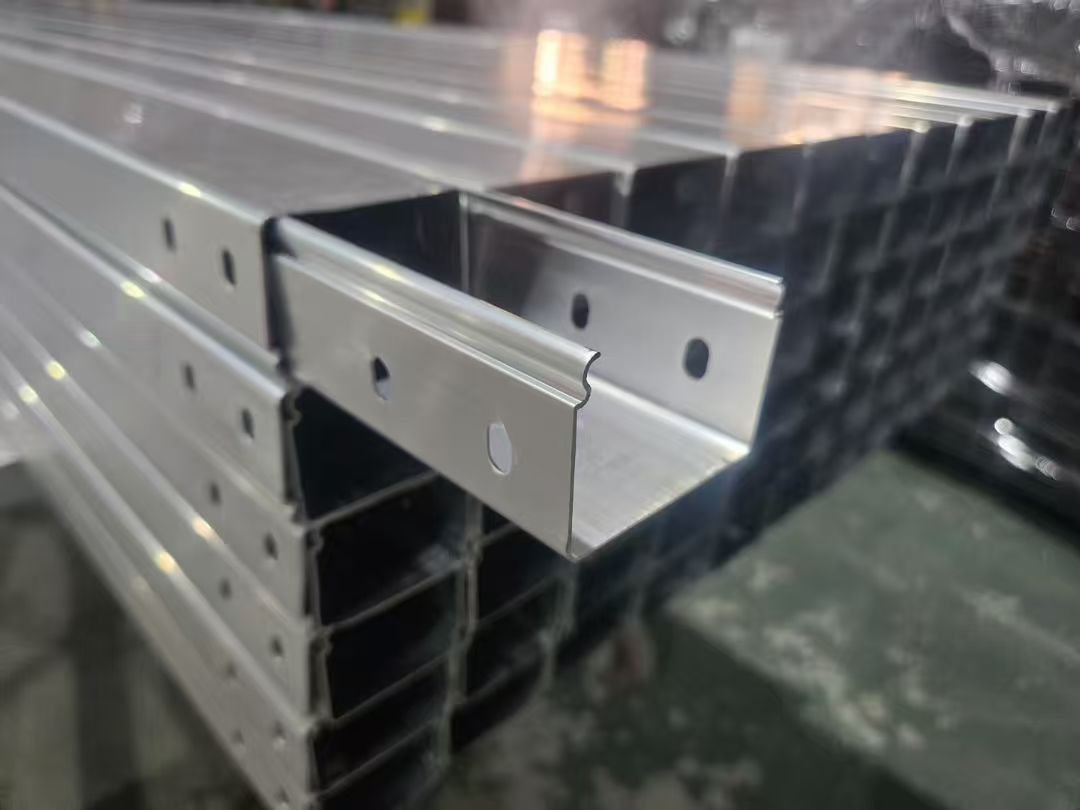
The core idea is simple. Instead of drilling, welding, or bolting at every joint, the tray body itself carries the fastener. The extrusion die shapes a locking profile directly into the 6063 aluminum alloy 1 section. When two parts meet, the geometry does the work.
The locking sequence, step by step
A typical self-locking joint follows a clear path. First, the installer positions the tray section on its supports. Second, the locking edge aligns with the matching groove. Third, a sliding or pressing motion engages the slider. The slider travels along a straight section, rides up a sloping section, and then snaps into a locking hole. Finally, an anti-locking section blocks the slider from backing out. This is a true boltless connection.
Component breakdown
| Component | Function |
|---|---|
| Tray body / channel | Carries and protects the cables |
| Locking profile or groove | Shaped feature that receives the slider |
| Slider / press-fit connector | Engages the groove and completes the lock |
| Cover or access lid | Clips on for protection and easy inspection |
| End caps and transition plates | Finish runs and connect to other systems |
Why die precision decides everything
Here is the point I stress with every buyer. The lock depends entirely on extrusion tolerance. If the die wears or the tolerance drifts, the clip either will not press in or will not hold tight. A bolt you can re-tighten. A failed clip you cannot. Good designs also leave engineered clearance at the locking interface so the run can handle longitudinal thermal expansion without stress. Some newer profiles even include internal geometric channels that can house fiber-optic sensing cables for real-time thermal and load monitoring.
What advantages does self-locking design offer over traditional bolted cable trays?
Every quarter I weigh the same trade-off with buyers: pay a bit more for boltless profiles, or stay with cheap bolted trays and absorb the labor cost on site.
Self-locking design cuts installation time by up to 50%, removes loose nuts and bolts, creates a snag-free interior for cable pulls, and keeps consistent metal-to-metal contact for electrical grounding. Traditional bolted trays need more tools, more hardware, and more labor at every joint.
The clearest way to see the difference is side by side.
| Factor | Self-locking aluminum tray | Traditional bolted tray |
|---|---|---|
| Joint hardware | None at straight-section joints | Nuts, bolts, splice plates at every joint |
| Installation time | Up to 50% faster, fewer tools | Slower; each joint is torqued by hand |
| Interior surface | Snag-free, no protruding hardware | Bolt heads can abrade cable jackets |
| Grounding path | Consistent metal-to-metal contact at locked joints | Depends on splice hardware and torque |
| Field adjustment | A failed clip cannot be re-tightened | A loose bolt can be re-torqued |
| End of life | Tool-less disassembly, clean material recovery | Slower teardown, mixed hardware waste |
Where the gains come from
Installation efficiency is the headline. On a long run, hundreds of bolted joints disappear. Fewer loose parts also means fewer dropped fasteners, fewer missed torque checks, and fewer installation errors. The snag-free interior matters during high-tension wire pulls, because there are no bolt heads to abrade cable jackets. And because the aluminum itself is highly conductive, the locked joints support the tray’s role as an integrated equipment grounding conductor. The non-magnetic material also prevents hysteresis losses around high-current circuits, which reduces heat buildup.
The honest objections
Buyers raise two fair objections. First, lock profiles are usually proprietary, so mixing vendors mid-project gets messy. My answer: standardize one supplier per system, and lock spare sections into the first order. Second, a bolt can always get one more turn; a clip cannot. That is true, and it is exactly why factory tolerance control matters more here than with bolted trays. Choose the factory, not just the product. One more upside worth noting: tool-less disassembly gives you uncontaminated aluminum at end of life, which recycles at high value.
Is self-locking aluminum alloy cable tray suitable for my industrial or solar project?
A project director in Singapore messaged me on WhatsApp last month with one blunt question: will this tray survive his rooftop solar site? My honest answer was: it depends.
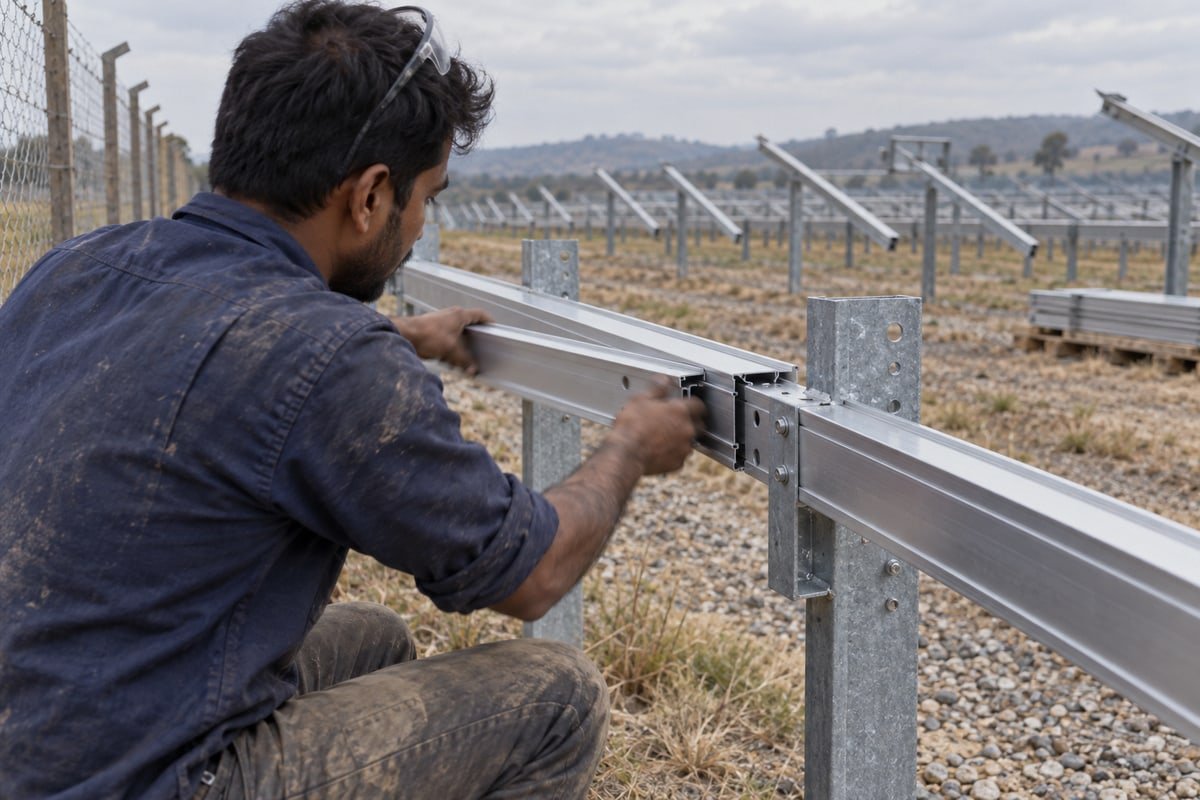
Self-locking aluminum alloy cable trays suit data centers, commercial complexes, factory buildings, and solar farms where light weight, corrosion resistance, and fast installation matter. For chemical corrosion workshops or humid underground tunnels needing full sealing, gasketed trough-type trays remain the safer choice.
I never tell a buyer this product fits everywhere, because it does not. The self-locking design solves the “install fast, never loosen” problem. It does not solve the “absolute sealing” problem. Match the tray to the environment, not the marketing.
Suitability by environment
| Environment | Fit | Why |
|---|---|---|
| Data centers and server rooms | Excellent | Non-magnetic, clean routing, easy access |
| Commercial complexes | Excellent | Fast installation, light structural load |
| Standard factory buildings | Good | Corrosion resistance 3, easy maintenance |
| Rooftop and ground-mount solar | Good | Light weight eases handling; oxide layer resists weather |
| Coastal or marine sites | Good | Copper-free 6063 aluminum alloy resists salt air |
| Chemical corrosion workshops | Poor | Needs fully sealed, gasketed trough-type tray |
| Humid underground utility tunnels | Poor | Needs full enclosure and sealing gaskets |
The solar case in detail
Solar EPC teams are our most frequent buyers for this profile, especially in Southeast Asia. The logic is strong. Rooftops punish heavy steel; aluminum’s strength-to-weight ratio reduces demands on supports. The self-healing oxide layer handles rain, humidity, and coastal air without paint or galvanizing. And boltless joints speed up repetitive long runs between strings and inverters.
Still, do the engineering. Verify load-bearing capacity 4 against your cable fill, and confirm the support span your spans actually allow. For very heavy feeder runs over long spans, a ladder type cable tray with verified load ratings may serve you better than any self-locking channel. Ask your supplier for load charts before you commit, not after.
How do I choose a reliable supplier for self-locking aluminum alloy cable trays?
I learned my hardest sourcing lesson early: a self-locking tray from a factory with worn dies simply will not lock. No amount of site adjustment can fix that.
Choose a supplier with proven extrusion die precision, documented tolerance control, 6063 aluminum alloy certificates, and load testing to NEMA VE 1 standards. Verify samples before bulk orders, confirm lead times in writing, and check their record on customization, QC, and export logistics.
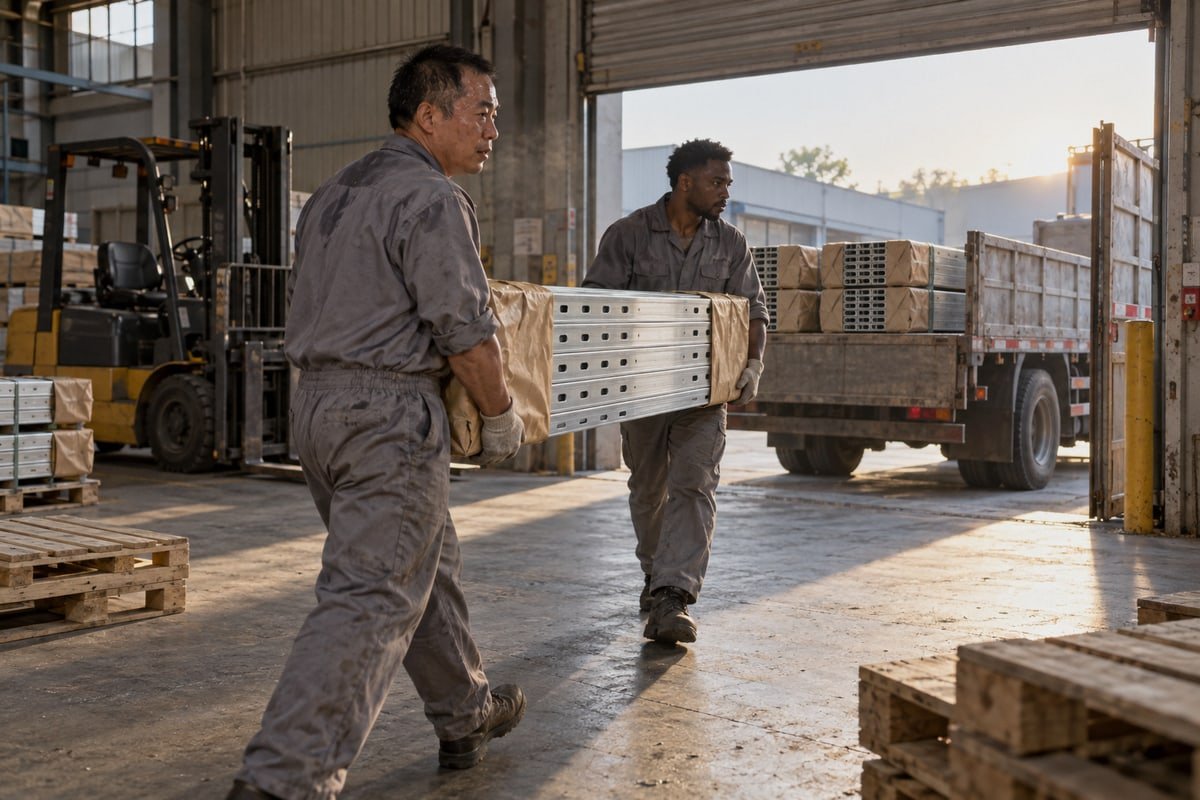
With bolted trays, an average factory can get away with sloppy tolerances. With self-locking trays, it cannot. The mold shop and the QC bench decide whether your project succeeds. Here is the vetting process I recommend to every EPC project manager and procurement lead, based on how we run things at LANYE CABLETRAY and what our buyers in Singapore, the Philippines, Thailand, and South America check before ordering.
- Test physical samples first. Lock two sample sections together yourself. Then try to pull them apart. A good joint engages with firm hand pressure and resists reverse movement completely. If the sample feels loose or refuses to seat, walk away.
- Ask about die maintenance. Extrusion dies wear over time. A serious factory tracks die life and measures locking-groove dimensions batch by batch. Ask how often they inspect and replace dies.
- Demand material traceability. Request mill certificates confirming 6063 aluminum alloy. Copper-free alloys matter for marine and coastal jobs.
- Check load documentation. Ask for load-bearing capacity data tested against NEMA VE 1 standards, with clear support span assumptions. Vague brochures are a warning sign.
- Verify electrical continuity. Consistent metal-to-metal contact at the locked joints should support electrical grounding. Ask for continuity test results across assembled joints.
- Confirm lead times and logistics in writing. Delivery delays kill project schedules. Get committed production and shipping dates into the contract, plus a plan for replacement sections, since lock profiles are proprietary.
- Assess customization ability. Projects rarely fit catalog sizes. A supplier offering OEM/ODM development can adapt widths, depths, and accessories to your drawings.
Our own team in Tai’an learned to pre-assemble random joints from every production batch before packing. It slows shipping by a few hours. It has saved buyers from opening containers full of trays that will not lock.
Conclusion
Loose bolts waste time and invite failure. A self-locking aluminum alloy cable tray solves that for standard environments — if the supplier’s dies and quality control are truly up to standard.
Footnotes
- Authoritative material specification for the aluminum alloy used in high-quality cable tray extrusions. ↩︎
- ISO 9001 certification ensures the factory maintains the strict tolerance control required for precision self-locking joints. ↩︎
- ISO 9223 is the international standard for classifying the atmospheric corrosion resistance of metals like aluminum. ↩︎
- NEMA VE 1 is the primary industry standard for testing the load-bearing capacity of metal cable trays. ↩︎